
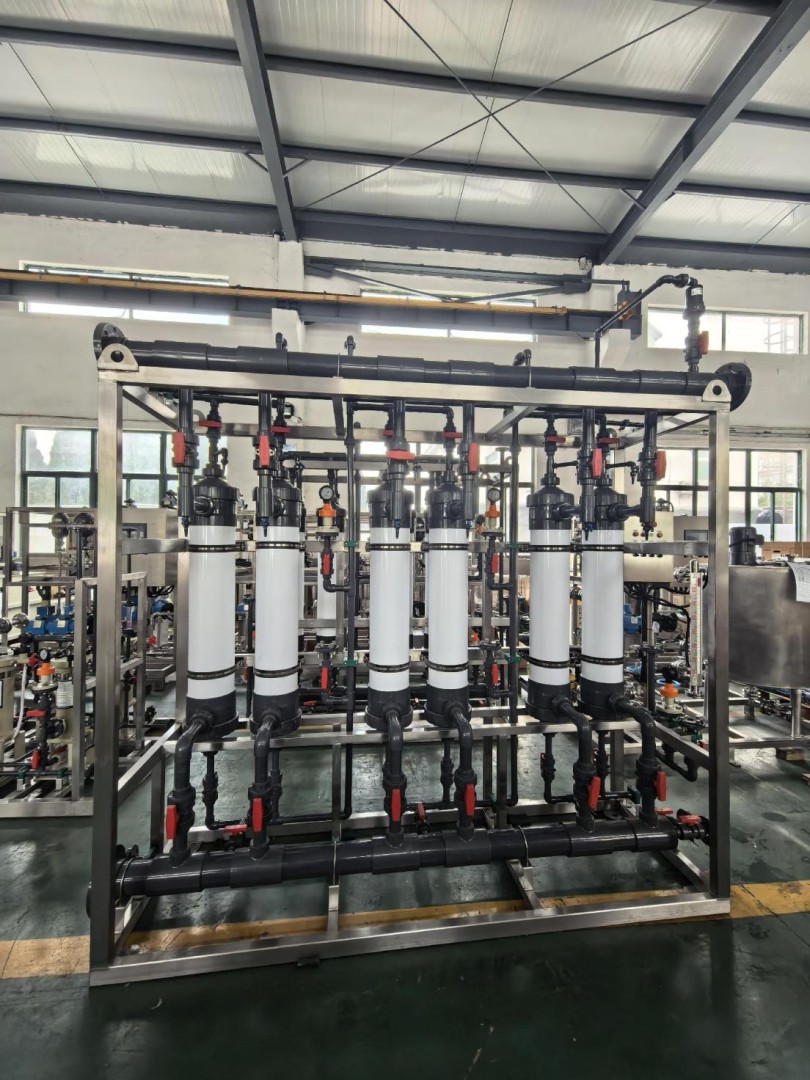
Shanghai, China – October 16, 2026 – QILEE (Qilee Group), a global provider of advanced industrial and municipal water treatment solutions, today announced the introduction of its Integrated Containerized PTFE Membrane Ammonia Stripping Unit. Designed to address severe high-concentration ammonia-nitrogen wastewater across heavy process industries, this compact, skid-mounted system offers a continuous 14 cubic meters per day (CMD) treatment capacity while enabling closed-loop resource recovery through waste valorization.
As environmental discharge mandates tighten globally, industrial manufacturers face mounting operational hurdles when managing ammonia-rich effluents. Conventional air-stripping towers and steam-stripping systems often require substantial real estate, heavy civil engineering, and intensive thermal energy, while merely migrating volatile pollutants between phases. QILEE’s modular membrane contactor technology redefines this workflow by coupling hydrophobic polytetrafluoroethylene (PTFE) hollow-fiber membranes with transmembrane chemical absorption, lowering ammonia levels and yielding a commercially viable 20% aqueous ammonia byproduct.
Breakthrough PTFE Membrane Contactor Technology
At the core of the unit is a transmembrane chemical absorption mechanism utilizing proprietary hydrophobic, porous PTFE hollow-fiber membranes. Compared to conventional polymers such as polypropylene (PP) and polyvinylidene fluoride (PVDF), PTFE exhibits superior resistance to harsh acids, strong alkalis, and aggressive organic compounds, ensuring extended membrane life in corrosive operating environments.
The operational sequence follows a continuous four-stage cycle managed through seven integrated modules:
- Pretreatment and Conditioning: Incoming raw wastewater enters through a dedicated security filter to remove suspended solids. A 40% sodium hydroxide (NaOH) dosing system raises the stream’s pH above 11.5, shifting dissolved ammonium ions ($NH_4^+$) into gaseous ammonia ($NH_3$). A plate heat exchanger adjusts the influent temperature to an optimal 35–45°C.
- Membrane Separation and Mass Transfer: The conditioned wastewater routes through the tube side of the PTFE membrane contactor. Due to the hydrophobic nature of the pores, liquid cannot penetrate, creating an undisturbed gas-liquid interface where gaseous ammonia diffuses rapidly across the membrane wall.
- Absorption and Valorization: Concurrently, chilled deionized (DI) water circulates through the shell side, absorbing the diffusing ammonia vapor to form ammonium hydroxide (aqueous ammonia).
- Discharge and Collection: The de-ammoniated effluent is safely discharged or transferred downstream for subsequent polishing. Meanwhile, the aqueous ammonia solution is continuously circulated until it achieves a target concentration of 20%, after which it is routed to dedicated storage for commercial reuse or on-site recovery.
High-Performance Specifications and Operating Parameters
The system is engineered for industrial-scale duty with continuous 24/7 operating capabilities, while maintaining low electrical and utility demands:
- Treatment Capacity: 14 m³/day (continuous 24-hour operation rating; baseline operating costs modeled at 8 hours/day, 260 operating days/year).
- Influent Resilience: Handles high-ammonia influent streams up to 35,000 mg/L.
- Discharge Quality: Achieves an effluent ammonia-nitrogen concentration of 40 mg/L or lower in a single stage, with multi-stage configurations available in series for ultra-low discharge requirements.
- Compact Footprint: Requires approximately 60 m², cutting land use substantially compared to tall, conventional stripping towers.
- Energy Consumption: Designed for an AC 380V/220V three-phase, five-wire electrical feed, the unit has a total installed power capacity of 23.94 kW, while drawing just 9.09 kW under standard operating conditions.
- Cleaning and Maintenance: Includes an automated flush and clean-in-place sequence consuming approximately 1,000 liters of tap water per cleaning cycle.
Turnkey Modular Skid and Intelligent Automation
Fabricated, pre-piped, and pre-commissioned at the factory, the system significantly reduces civil work schedules and capital expenditure. The containerized footprint permits rapid installation, easy relocation, and drop-in integration for plant expansions, overseas sites, or retrofits.
Process safety and stability are managed via an integrated Siemens PLC control system. The platform continuously tracks critical operating metrics, including pH, pressure differentials, fluid temperatures, and tank levels, and features automatic dosing, self-acting flush routines, and proactive alarms, minimizing on-site operator oversight.
Under QILEE’s deployment scope, the company supplies, installs, and commissions all primary equipment, process instrumentation, valves, internal piping, and automated panels inside the containerized skid, alongside hands-on operator training and technical documentation. Facility owners provide external utility tie-ins, foundation civil works, chemical supply, and on-site crane lifting.
Target Markets and Proven Industry Precedents
QILEE’s membrane stripping architecture is engineered to serve high-ammonia wastewater challenges across major process industries, backed by demonstrated field deployments:
- Mining and Metallurgy: Efficient treatment of mineral processing streams from vanadium and titanium extraction (validated by reference installations treating up to 280 metric tons per day of vanadium ore wastewater).
- Pharmaceuticals and Fine Chemicals: Management of complex organic synthesis and pharmaceutical manufacturing effluents (supported by commercial reference projects processing 300 metric tons per day).
- Pesticides, Dyes, and Intermediates: Robust degradation resistance against high-concentration textile printing, dyeing, and agrochemical intermediate effluents (demonstrated in 100 metric ton per day pesticide facilities).
- Petrochemical, Paper, and Fermentation: Tailored solutions for printing ink formulation, paper mills, and industrial food fermentation processes.
For inquiries, contact:
Website: http://qileegroup.com/
Email: tina@qileegroup.com
WhatsApp: +86 13636655908
Telephone: +86 13370035529
About QILEE
QILEE is a leading global provider of integrated, containerized water treatment systems. The company specializes in the design, engineering, and deployment of advanced modular solutions including MBR, UF, and RO processes, serving municipal, industrial, and remote water supply projects worldwide. With over 20 years of experience, 5,000+ successful projects, and 34 patents, QILEE has established itself as a trusted innovator in modular water treatment, delivering reliable, scalable, and sustainable clean water systems across more than 50 countries.
Media Contact
Company Name: QILEE
Contact Person: Tina
Email: Send Email
Phone: +86 13370035529
City: Shanghai
Country: China
Website: qileegroup.com
Press Release Distributed by ABNewswire.com
To view the original version on ABNewswire visit: QILEE Unveils Containerized PTFE Membrane Ammonia Stripping System for High-Strength Wastewater Resource Recovery